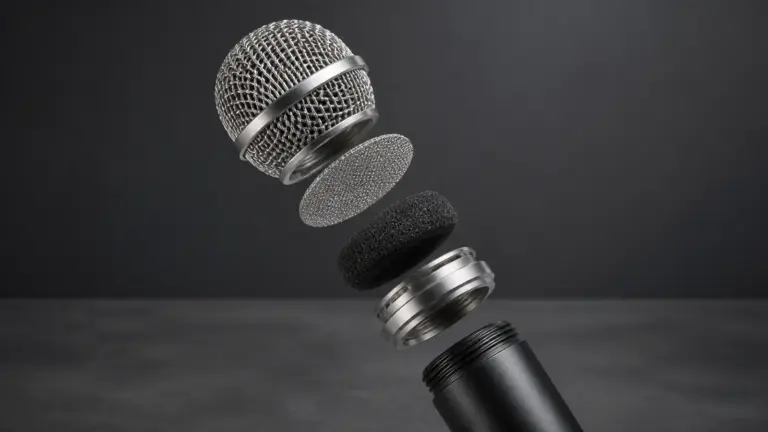
Before tooling a microphone housing, five areas should be confirmed: product structure, material and manufacturing process, critical dimensions and tolerances, assembly interfaces, and cosmetic acceptance standards. When these requirements are clear and measurable, the tooling supplier can evaluate the mold correctly, reduce post-trial revisions, and control assembly risk during mass production.
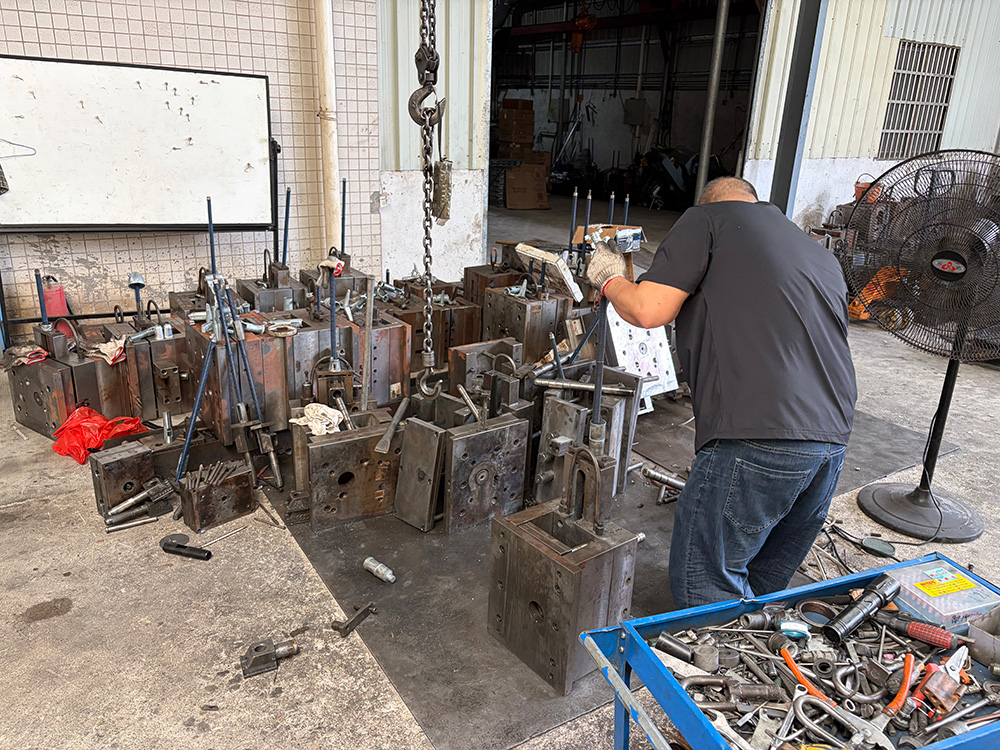
Tooling is not simply the conversion of a 3D model into a mold. A handheld microphone housing may need to accommodate the capsule, PCB, batteries, antenna, switches, display, and connectors while also meeting requirements for grip, acoustics, surface finish, and production-line assembly. For that reason, the decisions made before tooling often have a greater impact than the tooling process itself.
1. Have the Product Application and Internal Structure Been Finalized?
Housing requirements vary significantly between microphone categories. Even when two microphones have similar external dimensions, a wired microphone, wireless microphone, conference microphone, and entertainment microphone may require very different internal layouts.
What product information should be confirmed before tooling?
The project team should first confirm:
- Whether the product is wired or wireless
- Whether it is intended for stage performance, conferences, karaoke, streaming, or home entertainment
- Whether it uses a dynamic capsule, condenser capsule, or another transducer structure
- Whether it includes a display, adjustment buttons, mute switch, or lighting components
- Battery type, quantity, and installation direction
- Whether the antenna is internal, external, or integrated into the housing structure
- Whether the connector is XLR, USB, USB Type-C, or another interface
- Whether the product must be opened for servicing or battery replacement
- Target weight, grip diameter, and overall center of gravity
These decisions directly affect internal cavities, ribs, screw bosses, snap features, openings, and the way the housing is divided into separate parts.
For example, a wireless microphone housing usually needs to accommodate the battery compartment, PCB mounting features, and an RF antenna zone at the same time. If tooling begins before the electronics are stable, a later change to PCB dimensions or antenna location may require core inserts to be modified or, in more serious cases, part of the mold to be remade.
When can the structure be considered frozen?
A design freeze does not mean that no minor detail can ever change. It means the following fundamentals are no longer expected to change in principle:
- Overall product shape and major dimensions are fixed
- Installation space for the electronic components is confirmed
- The assembly sequence has been verified
- The position and orientation of major interfaces are fixed
- The housing split and parting strategy have been approved by the project stakeholders
Before releasing the mold, it is advisable to complete a full assembly using 3D-printed parts, CNC samples, or a functional prototype. Digital models can identify interference, but physical samples are usually more effective at revealing grip issues, assembly-access limitations, and insufficient service space.
2. Do the Housing Material and Manufacturing Process Match the Product Requirements?
Material selection should not be based only on appearance or unit price. The material affects product weight, structural strength, RF performance, finishing options, mold construction, and production consistency.
How should common microphone housing materials be selected?
Common materials for handheld microphone housings include:
- Zinc alloy: Provides noticeable weight and is suitable for die casting, including relatively complex shapes and curved surfaces.
- Aluminum alloy: Lower in weight and often used for drawn tubes, CNC-machined parts, or die-cast components. It is also suitable for anodizing.
- ABS plastic: Supports efficient molding and flexible structural design, making it suitable for products with tighter weight or cost targets.
- PC or PC+ABS: Suitable for plastic components that require improved impact resistance or specific cosmetic effects.
- Steel or stainless steel: Commonly used for grilles, mesh heads, decorative rings, and localized structural components.
No single material is suitable for every microphone project. The decision should consider product positioning, target weight, drop-test requirements, RF design, and the intended surface appearance.
A metal housing can provide a solid feel and good structural strength, but a wireless microphone also requires attention to antenna performance and grounding. Plastic is generally more transparent to RF signals, but wall thickness, sink marks, warpage, and surface wear must be evaluated carefully.
What process conditions must be confirmed after the material is selected?
The material and finishing process should be reviewed together, including:
- Die casting, injection molding, stamping, drawing, or CNC machining method
- Whether the wall thickness is suitable for the selected process
- Required draft angles
- Undercuts and whether slides or lifters are required
- Whether the finish will be painting, plating, powder coating, or anodizing
- Compatibility between the material and the target color, gloss, and texture
- Whether the surface finish will affect assembly dimensions
- Potential color or texture differences between dissimilar materials
A common project issue occurs when the structural design is completed first and the material is changed later. Plastic, zinc alloy, and aluminum alloy have different forming characteristics, so the original wall thickness, radii, ribs, and snap features may not transfer directly from one material to another.
The main material and manufacturing route should therefore be selected before mold design begins, rather than discussed only after the first trial.
3. Are Critical Dimensions, Tolerances, and Inspection Datums Clearly Defined?
A microphone housing may look acceptable but still fail in production if critical dimensions do not have defined tolerances. Typical results include components that cannot be installed, loose assemblies, sticking buttons, or visible mismatch between upper and lower housing sections.
Which dimensions are normally critical?
Dimensions that usually require closer control include:
- Diameter, depth, and concentricity of the capsule mounting area
- Positions of PCB locating posts and screw bosses
- Length, width, and contact allowance in the battery compartment
- Relationship between the display window and the display module
- Clearance for switches, buttons, and rotary controls
- Opening positions for XLR, USB, charging, or other connectors
- Fits between upper and lower housings, end caps, grilles, and decorative rings
- Groove dimensions for seals or shock-isolation components
- Dimensions that affect overall straightness and concentricity
These dimensions do not automatically require extremely tight tolerances. Tighter tolerances normally increase tooling, processing, and inspection costs and may also reduce production yield.
A more practical approach is to distinguish between:
- Functional dimensions
- Assembly dimensions
- Cosmetic dimensions
- General reference dimensions
Dimensions that directly affect function and assembly should receive the closest control. Dimensions with little functional impact can normally use production-appropriate general tolerances.
Why are common measurement datums necessary?
If the product designer, housing manufacturer, and assembly plant use different measurement references, the same feature may produce different inspection results.
The 2D drawing should define the following before tooling:
- Primary, secondary, and tertiary datums
- The datum from which each critical dimension is measured
- How the center axis of a cylindrical housing is established
- Whether acceptance is based on the part before or after finishing
- How warpage, straightness, and concentricity will be measured
- Whether acceptance is based on the individual part or the assembled product
A tolerance stack-up analysis is also important for housings made from multiple components. Individual parts may all be within tolerance while the final assembly is still unacceptable. Accumulated variation across the upper housing, lower housing, decorative ring, PCB, buttons, and display can create visible misalignment.
4. Have the Assembly Interfaces and Functional Requirements Been Verified?
The housing is part of the complete microphone system, not an isolated cosmetic component. Every interface should be reviewed from the perspective of final assembly and actual use before tooling begins.
Which assembly interfaces require particular attention?
The housing supplier, electronics engineer, and assembly plant should jointly verify:
- Whether the capsule can be located securely
- Whether adequate space is maintained between the capsule and grille
- Whether the PCB can be inserted and removed without excessive difficulty
- Whether screwdrivers and assembly tools have sufficient access
- Whether batteries can be installed and replaced smoothly
- Whether battery contacts have sufficient compression allowance
- Whether switches and buttons have suitable travel
- Whether the display is likely to shift or be compressed
- Whether the housing can withstand connector insertion and removal forces
- Whether wires or flat cables could be pinched during assembly
- Whether special fixtures will be required on the production line
- Whether servicing requires snap features or cosmetic parts to be damaged
Assembly design should also take production cycle time into account. A component that can be adjusted slowly during prototyping may become a significant bottleneck during volume assembly.
Are acoustic, RF, and reliability requirements included in the mechanical design?
A handheld microphone housing may also need to address:
- Capsule shock isolation and reduction of handling noise
- Acoustic spacing between the grille and capsule
- Noise caused by internal wire movement
- Grounding and shielding for metal housings
- Antenna clearance zones in wireless microphones
- Heat dissipation and ventilation
- Protection against dust, perspiration, or basic splashing
- Retention of batteries, PCB, and connectors after a drop
These requirements should not be checked only after pilot production. Structural samples, functional prototypes, and a joint assembly review can identify many of the risks before mold release.
5. Are the Cosmetic Standards and Acceptance Methods Documented?
“The appearance should look good” is not an executable inspection standard. Different people may have different expectations for color variation, parting lines, sink marks, and surface particles. Without agreed criteria, the mold-trial stage can become a cycle of repeated and subjective revisions.
What should be included in cosmetic confirmation?
A CMF document or cosmetic specification should define:
- Product color and approved reference sample
- Surface gloss level
- Texture, blasting, or molded-grain effect
- Painting, plating, or anodizing requirements
- Logo position, size, and manufacturing method
- Classification of cosmetic and non-cosmetic surfaces
- Acceptable parting-line positions
- Permitted locations for gate, ejector-pin, and slide marks
- Acceptance criteria for color variation, scratches, particles, exposed base material, and dents
- Color-consistency requirements between production batches
A logo may be applied by screen printing, pad printing, laser marking, etching, stamping, or molded-in features. Each method has different implications for the material, finish, and mold structure, so the logo process should also be confirmed before tooling.
How can cosmetic disputes after the mold trial be reduced?
Practical methods include:
- Providing a physical color sample rather than relying only on an on-screen color value
- Preparing an approved master sample or limit sample
- Marking the primary cosmetic surfaces on the drawing
- Confirming parting-line and gate locations during the mold review
- Defining whether inspection is performed under natural light, a standard light booth, or another condition
- Defining acceptance requirements for both individual parts and the fully assembled product
For metal housings, the effects of polishing, blasting, and surface finishing on edges, holes, and mating dimensions must also be considered. The higher the cosmetic requirement, the more important it is to reserve appropriate processing allowances during design.
What Information Should Be Prepared Before Tooling a Microphone Housing?
A complete tooling package normally includes:
- 3D structural files
- 2D drawings with critical dimensions and tolerances
- Product exploded view
- Electronic component drawings or physical samples
- Assembly-sequence instructions
- Material specifications
- Surface-finish and color requirements
- Logo files and processing requirements
- Functional test requirements
- Drop, abrasion, or environmental test requirements
- Cosmetic acceptance standards
- Approved samples or reference products
- Estimated order volume and production-batch plan
The 3D file is primarily used for mold design and structural analysis. The 2D drawing defines dimensions, tolerances, materials, and acceptance conditions. A 3D file without corresponding 2D technical requirements is normally insufficient for stable volume production.
Recommended Confirmation Process Before Tooling
To reduce the likelihood of mold revisions, a project can follow this sequence:
- Confirm product positioning and the internal electronics concept
- Complete the preliminary mechanical design
- Conduct a design-for-manufacturability review
- Produce 3D-printed or CNC structural samples
- Complete a full-product trial assembly
- Check acoustic, RF, and operating functions
- Confirm materials and surface finishes
- Freeze critical dimensions and interfaces
- Approve cosmetic standards in writing
- Review the mold design proposal
- Issue formal approval to begin tooling
For projects involving multiple suppliers, one controlled version of the drawings and bill of materials should be designated as the master. Every revision should carry a version number and date so that the housing manufacturer, electronics supplier, and assembly plant do not work from different files.
1. Can tooling begin with only a 3D file?
It may be technically possible, but it is not recommended. A 3D file normally does not fully define dimensional tolerances, material specifications, surface finishes, and inspection datums. Before tooling, it is preferable to provide 2D engineering drawings, assembly information, and cosmetic standards as well.
2. Can the housing mold be started before the electronics are fully finalized?
The risk is relatively high. At minimum, the PCB outline, battery space, capsule position, antenna zone, display, switches, and connector interfaces should be frozen. Changes to these items after tooling often require modifications to the core or inserts.
3. Is zinc alloy, aluminum alloy, or plastic the best material for a microphone housing?
The answer depends on the product. Zinc alloy is suitable when a solid weight and complex die-cast structure are required. Aluminum alloy is appropriate for lower weight, a metal finish, or anodizing. Plastic is useful when low weight, flexible internal geometry, or RF transparency is important. Surface finish, drop requirements, and target cost should also be included in the decision.
4. How can the number of mold revisions be reduced?
The most effective measures are an early design-for-manufacturability review, structural prototypes, a complete assembly test, and a joint tooling review involving the housing manufacturer, electronics engineer, and assembly plant. All parties should also use the same controlled versions of the drawings and component data.
5. Should every dimension have a tight tolerance?
No. Tolerances should be based on function and assembly needs. Unnecessarily tight tolerances can increase tooling, machining, and inspection costs. The strongest controls should be applied to capsule, PCB, battery, button, display, connector, and housing-mating dimensions.
6. Should mold ownership and maintenance responsibilities be confirmed in advance?
Yes. Before tooling, the contract or mold agreement should define mold ownership, storage location, maintenance responsibility, treatment of normal wear, modification costs, retention period after production stops, and conditions for mold transfer.
Conclusion
The central task before tooling is to convert product expectations into clear, measurable, and verifiable engineering standards. The more thoroughly the project confirms structure, materials and processes, dimensional control, assembly function, and cosmetic acceptance, the more focused the mold-trial adjustments will be and the easier it will be to maintain consistency in volume production.
ENPING SHUNFENG ELECTRONICE CO., LTD. has 20 years of experience manufacturing handheld microphone housings. Based on our project experience, a joint review of structure, assembly, and manufacturability before mold design is usually more effective than repeated revisions after the first trial. For projects that are still in development, validating structural samples and critical interfaces before selecting the final tooling solution is generally the more reliable approach.